Multiply the area the oil pushes on by the speed the cylinder needs to move. That gives the flow into the cylinder. To find the pump flow rate, add the demand from any other function that must run at the same time on that pump. Check the combined flow at the pump’s actual shaft speed and at the pressure the machine needs for that part of the cycle.
Use the full piston area when oil enters the end opposite the rod. Use the smaller area around the rod when oil enters the rod end. The two areas can give different flow requirements on the same cylinder, even when the stroke is the same length. If the valve uses a special circuit that redirects return oil, get the circuit drawing before applying the ordinary two-port calculation.
| Start with | It tells you |
|---|---|
| Cylinder bore and rod diameter | How much area the oil acts on in each direction |
| Travel and desired time | How quickly the cylinder must move |
| Other functions running at the same time | Which flows the pump may need to supply together |
| Actual pump shaft speed | How much a given pump displacement can deliver |
| Pressure for each movement | Which pump and drive rating must cover that flow |
The numbers below describe a hypothetical machine. They show how to build a flow requirement for a quote and how to read the answer. Actual cylinder dimensions, circuit behaviour and pump ratings should come from the equipment drawings and the supplier.
Start with the part of the movement that has a time limit
A cycle description might say that a cylinder must “complete its stroke in four seconds.” Find out where the clock starts. If the four seconds include a pause while a clamp closes, the cylinder may have less than four seconds to move. Separate the time spent moving from the time spent waiting. On an existing machine, use a position record or the approved sequence so the calculation reflects the travel the cylinder makes during that window.
Record travel in millimetres and time in seconds. The travel can be shorter than the cylinder’s full stroke. If a 700 mm cylinder moves only 500 mm on the working cycle, use 500 mm for the flow calculation and keep the full stroke on the equipment record. If there are separate fast and slow parts of that movement, list the travel and time for each. The fast approach and the working part can put different demands on the pump.
For the first estimate, treat the speed over that travel as steady. Divide travel by time. A 500 mm movement in 4 seconds gives an average speed of 125 mm/s. Convert it to metres per minute when using the metric formulas below. At 0.125 m/s, the cylinder travels 7.5 m/min. If most of the four seconds include acceleration and deceleration, ask the machine designer for the peak speed it intends to use. The average alone can understate the required peak flow.
For a repair, confirm what the machine did when it was operating correctly. A time measured after a speed problem arose can be useful diagnostic evidence, while the original cycle time gives the target for the replacement. Keep the two in separate columns. Also record whether the slow movement is extending, retracting or moving under load. That helps the supplier decide whether a new pump is the right subject of the inquiry or whether it needs more information about the circuit.
On a new build, the cycle target may come from production or from a timing requirement on the next machine in the line. Write that target against the actual position change. If the motion can be staggered without affecting the machine’s output, ask the controls designer which functions can be moved to a different time window. That changes what the pump has to supply together, and it can be checked before a pump is selected.
Which cylinder area should you use?
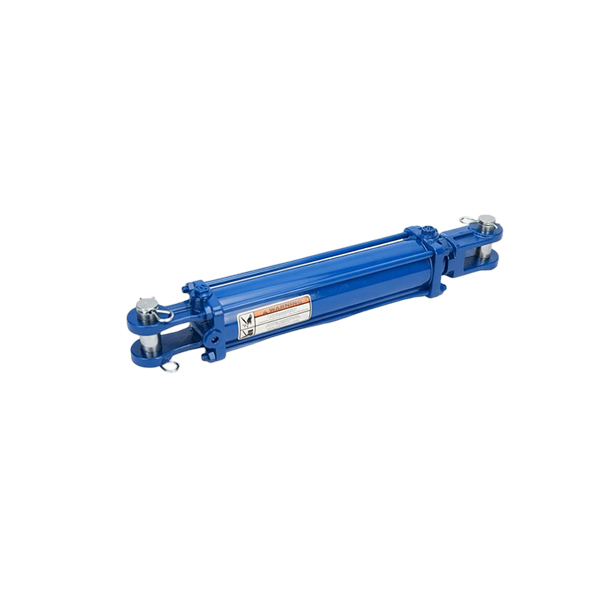
For a conventional double-acting cylinder, use the full piston area for extension. For retraction, subtract the rod’s cross-sectional area from the full piston area. Multiply the area for each direction by the required travel speed to calculate the flow into that chamber.
The bore is the cylinder’s inside diameter. The rod is the shaft that comes out of the cylinder. The ring of piston surface around it is called the annular area.
Use the bore and rod dimensions from a controlled drawing, the cylinder code or the equipment maker. The outside of the barrel is larger than the bore, so an outside measurement is not enough to identify the piston area. If the old cylinder has been replaced, compare the installed dimensions with the machine documentation. A change in the rod diameter can change the retraction flow even if the bore is the same.
With diameters in centimetres, use π × diameter² ÷ 4 for the area in square centimetres. If the drawing is in millimetres, divide both diameters by ten before calculating. Keep the unrounded areas for the flow calculation. The same area, speed and volume relationships are shown in Peninsular Cylinder’s hydraulic formulas.
An ordinary cylinder formula describes the oil volume entering the chamber that drives the motion. If the cylinder has a different arrangement, use the actual areas and flow paths. An example is a valve circuit that sends oil leaving the rod end back into the cap end during extension. That oil can contribute to the cap-end flow. The pump requirement and available pushing force in that mode depend on the circuit. Send the valve diagram and the mode timing to the supplier before it applies the ordinary cap-end calculation.
If a machine has two cylinders moving together, identify how the circuit divides the oil. A flow divider or a controlled valve can change the relation between a pump reading and the flow into each cylinder. Put each cylinder on the worksheet with its own dimensions and expected speed. Add the flows only when the cylinders actually move together under a circuit arrangement that calls for both flows from the same supply.
Worked example for a four-second extension and three-second return
Take a conventional cylinder with an 80 mm bore, 45 mm rod and 500 mm of travel. The assumed machine calls for extension in four seconds and retraction in three seconds. It uses the cap end to extend and the rod end to retract. The example ignores cylinder leakage and treats speed over each movement as steady. The pressure needed to move the load is a separate input.
Convert the diameters to 8 cm and 4.5 cm. The full piston area is π × 8² ÷ 4, or about 50.27 cm². The rod area is π × 4.5² ÷ 4, or about 15.90 cm². Subtract to get about 34.36 cm² at the rod end. Keep these two working areas on the sheet and use the applicable one on each movement.
To use area in cm² and speed in m/min, multiply the two numbers and divide by 10 to get L/min. One metre equals 100 cm, and one litre equals 1,000 cm³. That is where the factor of ten comes from. If you work in other units, convert the figures before using this version of the formula. The division by ten applies only to the units stated here.
Extension at 500 mm in four seconds is 7.5 m/min. Multiply 50.27 cm² by 7.5 m/min and divide by 10 to get about 37.7 L/min into the cap end. Retraction at 500 mm in three seconds is 10 m/min. Multiply 34.36 cm² by 10 m/min and divide by 10 to get about 34.4 L/min into the rod end. Round for the worksheet after the calculation.
| Movement in the example | Travel and time | Area used | Average speed | Oil entering the cylinder |
|---|---|---|---|---|
| Extend | 500 mm in 4 s | 50.27 cm² | 7.5 m/min | 37.7 L/min |
| Retract | 500 mm in 3 s | 34.36 cm² | 10 m/min | 34.4 L/min |
You can check the extension result another way. Over 50 cm of travel, the cap end takes 50.27 cm² × 50 cm = 2,513.5 cm³, or about 2.51 L. Delivering that volume in four seconds takes about 37.7 L/min. The volume method is useful when the drawing already shows the oil volume for the motion. It also gives the person reviewing the sheet a second route to the same number.
A change to retraction time changes the result. If the same 500 mm return must take two seconds instead of three, average speed becomes 15 m/min. The rod end then needs about 51.5 L/min in this example. In that case the return stroke would ask for more flow than the four-second extension. If a buyer speeds up only the return, update that row and see which movement now governs the pump requirement.

When do you add cylinder flows to size the pump?
Add the supply flows of functions that need oil from the same pump at the same time. For sequential movements, compare the flows in each time window and use the highest demand. Check flow priority and the pump pressure required during the overlap.
Imagine a second function that requires 12 L/min from the same pump during extension. If it is active while the cylinder needs 37.7 L/min, the two loads together ask for about 49.7 L/min at that time. If the second function runs after the cylinder stops, use separate rows. In that sequence the higher individual demand governs, subject to the way the circuit supplies the loads and any other demand the pump has to cover.
The timing can be easier to see on a plain table. Use one row for each period in which the set of active functions stays the same. Show when each function starts and ends. If you have the machine’s program or sequence chart, mark the source of the timing. If a function can start early because of an operator command, check whether that overlap is part of the required duty.
| Example time window | Active functions from the same supply | Flow used for a first review |
|---|---|---|
| Extension only | Main cylinder extends | 37.7 L/min |
| Part of extension with a second function running | Main cylinder and 12 L/min branch | 49.7 L/min |
| Return without a second function | Main cylinder retracts | 34.4 L/min |
Check the calculated demand against the valve diagram. If the circuit gives one function priority, mark the required speed of that function and whether the other can slow down. The supplier can then check the circuit against the actual sequence.
Pressure also belongs next to each flow row. Two branches at different loads can have different pressure requirements even when they share a pump. Record the pressure needed for each function and how the circuit supplies them. Avoid adding their pressures. Ask the designer or pump supplier which pressure the pump must reach when they run together, and record any pressure loss allowed through the valves and lines.
Mark any overlap the machine can do without. Controls may be able to delay a low-priority function until the heavy stroke ends, or the machine may need the two at the same time. A useful inquiry states that choice openly. It can also say what happens if the second function slows, such as a longer cycle with the required main-cylinder speed preserved. That tells the vendor what to protect when it compares options.
Check the peak speed if the cylinder ramps up and down
A four-second move is not always four seconds at the same speed. Suppose the cylinder starts at rest, speeds up evenly for half a second, holds speed for three seconds and slows evenly for the last half second. Each half-second ramp contributes the same travel as a quarter second at full speed. The 500 mm travel is therefore equivalent to 3.5 seconds at the peak speed. Divide 0.50 m by 3.5 s to get about 0.143 m/s, or 8.57 m/min.
At that speed, the 50.27 cm² cap end needs about 43.1 L/min. The earlier 37.7 L/min is the average over the four seconds. If the second branch takes 12 L/min during the full-speed portion, the estimated peak demand is 55.1 L/min. If it runs during a different part of the cycle, use the flow at that time. Mark the assumed speed profile on the worksheet. The controls engineer can replace it with the specified or recorded profile.
| Four-second extension in the example | Cylinder flow | What the number describes |
|---|---|---|
| Average over the full move | 37.7 L/min | The volume that enters the cap end over four seconds |
| Peak with the assumed ramps | 43.1 L/min | The cylinder’s flow during the full-speed part |
| Peak when the other branch runs at full speed too | 55.1 L/min | The combined requirement during that overlap |
Why can cylinder return flow be greater than pump flow?
During retraction, the pump feeds the smaller rod-end area while oil leaves the larger cap end. Both volumes change at the same piston speed. The cap end can therefore send more oil back through the valve than the pump supplies to the rod end.
During the three-second retraction in the example, the rod end takes about 34.4 L/min. Oil leaves the cap end at a rate set by the larger full piston area. At 10 m/min and 50.27 cm², that is about 50.3 L/min of return flow in the same ideal calculation. The return figure belongs on the valve and return-line review. It comes from the volume the piston pushes out of the cap end during the movement.
It helps to keep two columns on the same worksheet. One shows the oil supplied to the active chamber. The other shows the oil leaving the opposite chamber. During normal extension, the cap end takes 37.7 L/min and the rod end returns about 25.8 L/min at 7.5 m/min. During retraction, the rod end takes about 34.4 L/min and the cap end returns about 50.3 L/min at 10 m/min. Both calculations use the conventional circuit assumed here.
Check the actual return path in the drawing. The oil may pass through a valve, a filter, a cooler or another component on the way back. If several functions return at once, the shared path can see more than one return stream. Give the supplier the flow and temperature expected on that path. The maximum pump flow printed on a catalogue does not describe the return flow from every cylinder movement.
If an existing machine moves at the expected speed one way and slowly the other way, take note of which chamber supplies and which chamber returns in the slow direction. A pump reading is one part of the record. The valve position, timing, return conditions and load in that direction also matter. The BLINCE guide to hydraulic pump testing describes how measured flow, pressure and temperature help with an existing machine. Use the worksheet here to define the required flow before comparing a measurement with the target.
Turn required flow into a pump shortlist
Pump displacement is the volume the pump moves in one shaft revolution in the ideal calculation. Multiply displacement in cm³/rev by shaft speed in rpm and divide by 1,000 to get theoretical flow in L/min. Actual delivery will be lower than the ideal figure where internal leakage matters. To estimate delivery, multiply by the pump’s volumetric efficiency at the point you want to compare.
For a hypothetical pump with 32 cm³/rev at 1,500 rpm, ideal flow is 48 L/min. If you assume a volumetric efficiency of 0.90, estimated delivery is 43.2 L/min. That covers the 37.7 L/min extension in the example, with about 5.5 L/min left at that point. It comes short of the 49.7 L/min example with the second function running. Those comparisons assume the pump can maintain that efficiency and speed at the required pressure.
Try a second hypothetical displacement of 40 cm³/rev. At 1,500 rpm and the same assumed efficiency it would deliver 54 L/min. At 1,250 rpm it would deliver 45 L/min. One drawing may show both speeds at different operating conditions. Against the 49.7 L/min case, the 1,500 rpm estimate passes the flow check and the 1,250 rpm estimate falls short. Ask for the pump curve and the speed at the time of the actual movement.
| Hypothetical pump input | Estimated delivery at 0.90 efficiency | Does the estimate reach 49.7 L/min? |
|---|---|---|
| 32 cm³/rev at 1,500 rpm | 43.2 L/min | No |
| 40 cm³/rev at 1,500 rpm | 54 L/min | Yes, subject to pressure and duty checks |
| 40 cm³/rev at 1,250 rpm | 45 L/min | No |
These values are arithmetic examples. They do not describe the efficiency or availability of a BLINCE pump. Get delivery and efficiency information for the offered pump at the intended speed, pressure and oil conditions. The distinction between theoretical and actual delivery is also set out in Danfoss gear pump technical information.
A pump driven through a gear train may turn at a different speed from the engine or electric motor. Record pump shaft speed or provide the drive ratio and source speed. If the machine must work at idle, write down the speed at idle during the required motion. Also check the highest pump shaft speed and the applicable pump limits. Selecting a larger displacement to cover low speed can lead to more flow at higher speeds than the circuit was intended to handle.
If the equipment uses a variable-displacement pump, its maximum displacement gives one useful boundary. What it delivers at a particular moment also depends on the control and the demand seen by the pump. Describe the normal and peak operating points and the control arrangement in the inquiry. If the circuit caps flow or power under load, state the setting or supply the approved diagram. The largest number in the pump catalogue may be available only under specified conditions.
Pressure and power can narrow the shortlist further. For a simple hydraulic power estimate in metric units, multiply flow in L/min by pressure difference in bar and divide by 600. In a hypothetical point of 49.7 L/min at 140 bar across the pump, that gives about 11.6 kW of hydraulic output. The drive must also cover losses. Use the supplier’s efficiency data and the actual duty to review input power, shaft torque and the drive’s available power at the operating speed.
When the flow is known and the pressure is still open
Take a separate hypothetical force check on the same 80 mm cylinder. If the cap end has to push with 50 kN, and you neglect rod-end back pressure and friction for this first calculation, divide 50,000 N by the full piston area, about 0.005027 m². The result is about 99.5 bar at the cap end. Give the supplier the load direction and the pressure data for the actual circuit. Rod-end pressure, friction and line losses can change the pump pressure required. Keep the force estimate and the 140 bar example above on separate lines so one assumption does not become the machine’s quoted pressure.

Use the worksheet to compare a quote
Start with a short table that shows each movement, its travel and time, the active cylinder chamber, and the calculated flow. Attach the cylinder drawing and the circuit or sequence chart. Show the fastest allowed movement, the times that overlap, and the pressure expected at the pump during those periods. Include the pump shaft speed range and the fluid conditions expected at the machine.
When a quote gives only displacement, ask for the flow the pump is expected to deliver at your operating points. If the quote gives one delivery value, ask which speed, pressure and oil condition it represents. Record the proposed full pump code and drawing revision. A nameplate with the same displacement can leave open questions about the control, rotation, mount, shaft and ports.
| Ask the supplier to return | What you can check |
|---|---|
| Offered pump code, drawing and drive speed range | Whether the proposed configuration fits the drive |
| Delivery at the operating pressure and shaft speed | Whether the quoted pump covers the busiest part of the cycle |
| Power or torque requirement over the duty | Whether the machine drive can supply the pump |
| Control and pressure limits | How the pump behaves during the shared and high-load periods |
| Any open assumptions in the quote | Which drawing, measurement or cycle detail still needs confirmation |
Mark any figures still awaiting confirmation directly in the table. If the pump pressure during overlap is open, ask the vendor what circuit data it needs. Revisit those rows when the cylinder, timing or drive ratio changes.
Use the BLINCE hydraulic calculator for additional checks and the BLINCE hydraulic pump range to identify the family for an inquiry. Give the supplier the calculation inputs as well as the result. With the bore, rod, travel and timing visible, someone else can check the flow requirement if a drawing revision or cycle change comes through.
For the sample cylinder, a usable worksheet entry would read “Extend 500 mm in 4 s, 80 mm bore, cap end, 37.7 L/min average.” Add a second line for the peak if the controls specify a ramp. A separate column can show whether the 12 L/min branch overlaps the peak and who confirmed the timing. If nobody has confirmed the pump pressure during that interval, mark it open before sending the quote request.
Send the worksheet and drawings through the BLINCE Hydraulic inquiry page. Ask for the offered pump code, its delivery at the required speed and pressure, and the corresponding installation drawing. Ask the supplier to identify any missing conditions that could change those figures.